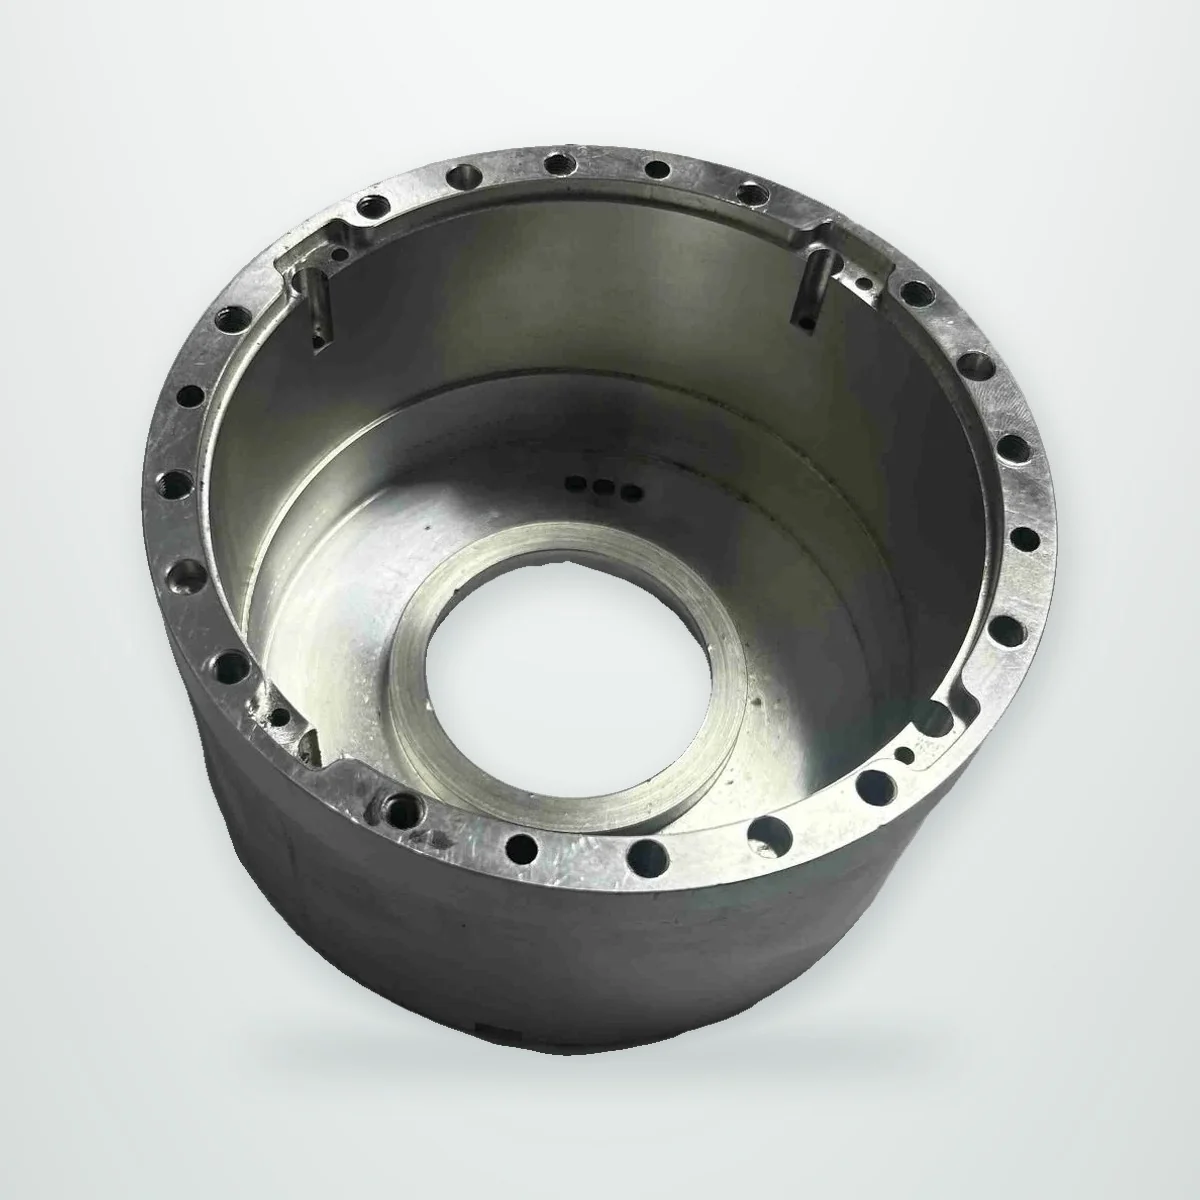
Aluminum
6061 · 6082 · 7075
Lightweight housings, brackets and fixtures.
Finish routes
Anodizing · Bead blasting
MATERIALS & FINISHES
6061, 6082 and 7075 aluminum, 304 and 316 stainless steel, 42CrMo4 alloy steel, brass and engineering plastics, with anodizing, passivation, plating and heat treatment. Balance strength, weight, environment, surface condition and manufacturing requirements. Confirm the grade and finish in the quotation.

MATERIAL SELECTION

6061 · 6082 · 7075
Lightweight housings, brackets and fixtures.
Finish routes
Anodizing · Bead blasting

304 · 316
Corrosion-exposed parts and rotational components.
Finish routes
Polishing · Passivation
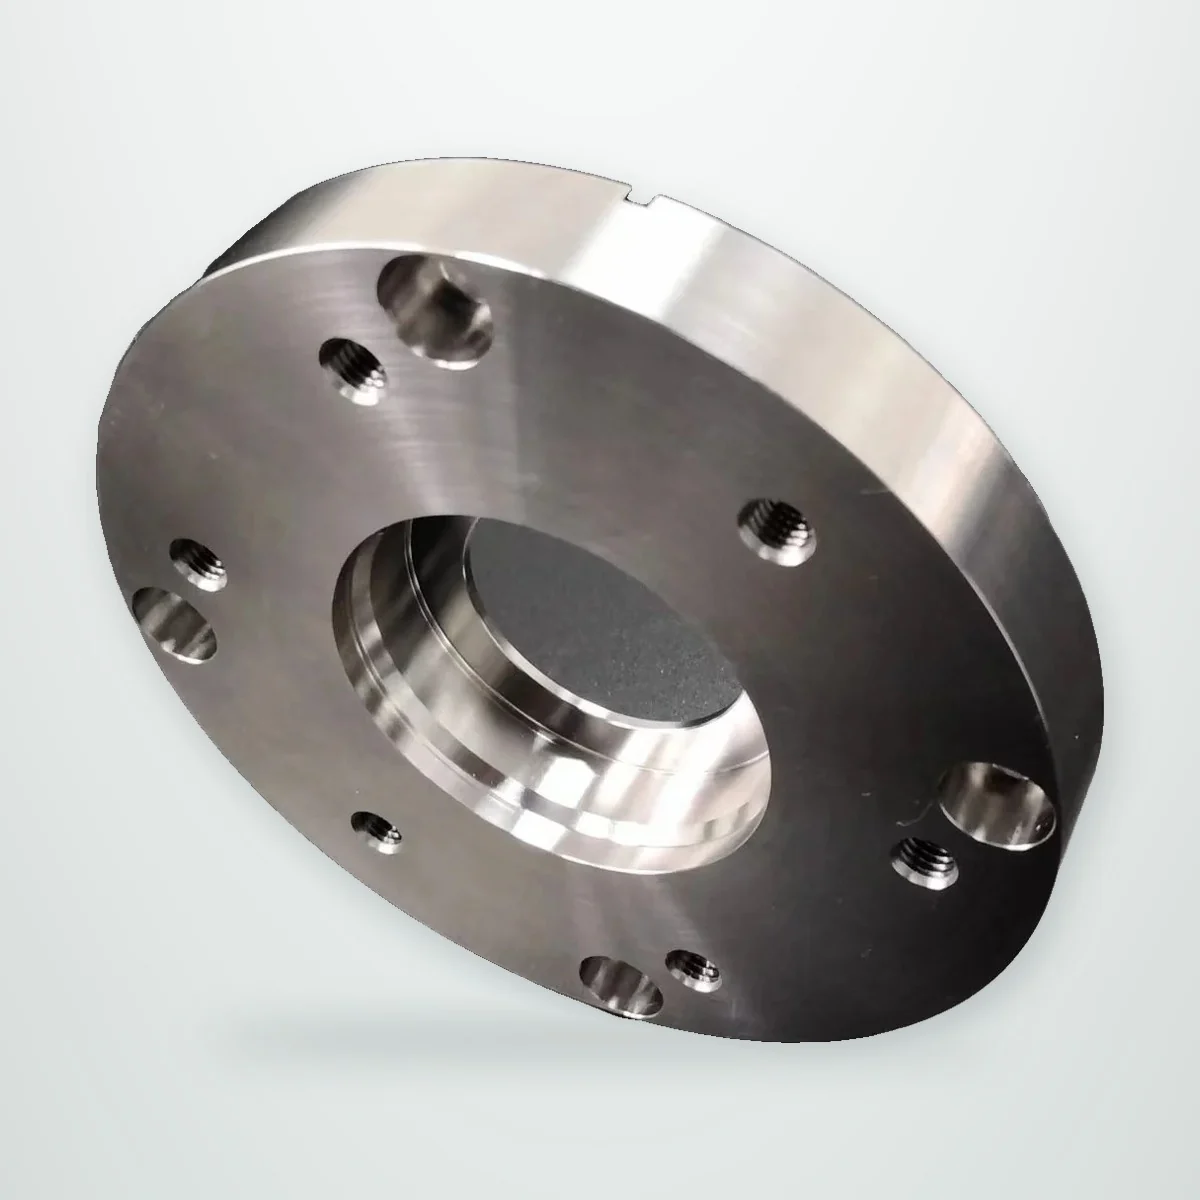
Grade per drawing
Load-bearing and wear-sensitive components.
Finish routes
Heat treatment · Coating

Alloy per application
Conductive parts, fittings and hardware.
Finish routes
Polishing · Plating
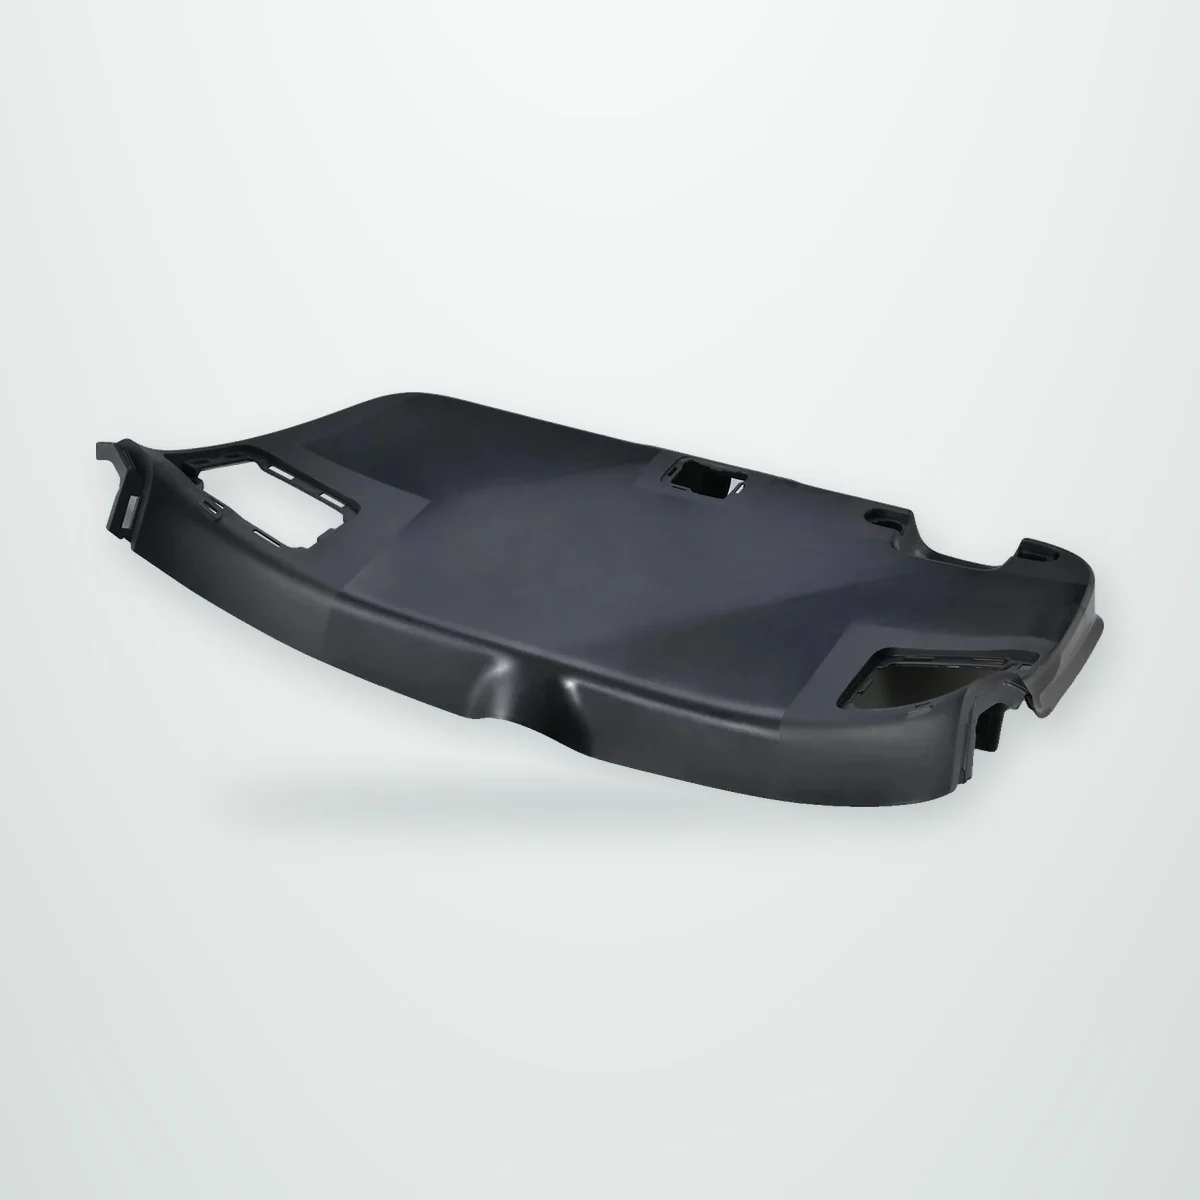
POM · PA · PC · PEEK
Insulating, lightweight and wear components.
Finish routes
Application-dependent finish

Grade per application
Functional molded components and cosmetic surfaces.
Finish routes
Tool texture · Color
No matching material. Try another keyword.
3D printing materials: resins, nylon, TPU, metals and ceramics

FINISH & DIMENSIONS
Finishing can affect dimensions, appearance and service performance. Review the complete specification before manufacture.
7075-T6 for high strength aluminum parts, 6061-T6 or 6082-T6 for general housings and plates.
304 or 316 stainless steel for wet or washdown environments, 17-4PH where strength is also needed.
Alloy steels with heat treatment for shafts, gears and locating pins.
POM, PA and PEEK for bushings, guides and insulating components.
Typical choices for robotics, automation and machine parts. EN, JIS or GB equivalents are quoted when your drawing calls for them.
| Material | Common grades | Typical parts | What to watch on the drawing |
|---|---|---|---|
| Aluminum, general | 6061-T6 / T651, 6082-T6 (EN AW-6082) | Housings, base plates, brackets, fixtures | Machines and anodizes cleanly. 6082 is the usual plate grade in Europe and is often accepted in place of 6061. |
| Aluminum, high strength | 7075-T6 / T651 | Robot links, joint housings, highly loaded brackets | Yield strength is roughly 1.8 times that of 6061-T6, but corrosion resistance is lower and hard anodizing can vary in color. |
| Stainless steel | 304 (1.4301), 316L (1.4404) | Washdown equipment, food and packaging machine parts, fittings | Work hardens while cutting, so thin walls and small holes take longer. Passivation after machining is usual. |
| Precipitation-hardening stainless | 17-4PH (1.4542) | Shafts, pins and valve parts that need strength and corrosion resistance | State the condition, for example H1025 or H1150. Parts are machined hardened or aged after machining. |
| Alloy steel | 42CrMo4 (AISI 4140), 40Cr | Shafts, gears, pins, couplings | Usually bought quenched and tempered at about 28 to 32 HRC and machined in that state. Induction hardening or nitriding can follow. |
| Case-hardening steel | 20MnCr5, 16MnCr5 | Gears and pinions that need hard teeth and a tough core | Carburized to about 58 to 62 HRC at the surface. Leave grinding stock on teeth and bearing seats when distortion matters. |
| Tool steel | D2 / SKD11 (1.2379), H13 (1.2344) | Locating pins, wear plates, punches, mold inserts | D2 is typically 58 to 62 HRC and H13 44 to 52 HRC after hardening, then ground or finished by wire EDM. |
| Brass | CW614N (C36000), H59 | Fittings, threaded inserts, connectors | Free machining with a fine finish. Ask for lead-free brass if the part touches drinking water or your customer limits lead. |
| Engineering plastics | POM-C, PA6, PEEK, PTFE | Bushings, guide strips, insulators, wear pads | POM is the stable default. PA absorbs moisture and grows. PEEK when temperature or chemicals rule the others out. |
Typical coating thickness per surface. On a bore or a shaft the diameter changes by about twice the outward growth, so a fit that measures correctly before finishing can be wrong after it.
| Finish | Typical thickness | Effect on fits and threads |
|---|---|---|
| Anodizing, Type II | 5 to 25 µm | About half grows outward. H7 bores and fine threads are masked or machined with an allowance. |
| Hard anodizing, Type III | 25 to 50 µm | About half grows outward, so a bore can lose 25 to 50 µm on diameter. Mask bearing seats or finish them after coating. |
| Electroless nickel | 5 to 25 µm | Very even, also inside bores and threads, so the allowance can be calculated closely. |
| Zinc plating | 5 to 12 µm | Builds up on edges and threads. Cut threads with a plating allowance, for example 6g, or mask them. |
| Black oxide | Under 1 µm | No practical effect on fits. Mild corrosion protection when oiled. |
| Passivation | None | Cleans stainless steel without changing dimensions. |
| Gas nitriding | A few µm of growth | Small growth and possible distortion on long parts. Critical journals can be ground afterwards. |
Worked allowances for H7 bores, g6 shafts and M6 threads are in the guide on anodizing allowances for bores, shafts and threads.
Part examples made to drawing: anodized aluminum pocket cases and a stainless steel drive shaft.
6061-T6 or 6082-T6 suits most housings, plates and brackets. 7075-T6 is worth its higher price where yield strength or stiffness to weight decides the size of the part, such as long links and thin-walled joint housings.
Yes. Quench and temper, case hardening, induction hardening and nitriding are planned with the machining route, and grinding stock is left on features that must hold size after heat treatment. Hardness is checked after treatment.
Yes. Material certificates traceable to the batch can be supplied when the order requires them.
Yes. Type II adds a few microns, while hard anodizing builds a thicker layer that can close up fits. Fit-critical bores are usually masked or finished after coating.
Often yes, for example EN or JIS equivalents of ASTM grades. Any substitution is proposed in the quotation and used only with your approval.
LET’S TALK ABOUT YOUR PART
Send the drawing and a line on how the part is used. We will suggest a material and finish and say what it means for the fits and the price. Or email the drawing to info@tovilon.com.