Anodizing grows a machined aluminum part. Bores and internal threads get smaller, shafts and other external features get larger, and the change is big enough to turn an H7 fit or a fine thread into a reject. This guide gives the growth for Type II and hard anodizing, worked allowances for bores, shafts and threads, how to choose between masking and pre-compensation, and the drawing notes that make the finished part fit.
Short answer.
- Internal features shrink, external features grow. Bores and tapped holes get smaller; shafts, pins and outside diameters get larger.
- A diameter changes by about the coating thickness. As a rule of thumb about half of the coating grows outward on each surface, so a bore with a 12 µm coating shrinks by about 12 µm. Confirm the actual growth with the anodizer.
- Typical thickness: Type II about 8 to 25 µm; Type III hard anodizing about 25 to 60 µm.
- Two ways to compensate: machine internal diameters oversize and external diameters undersize by the agreed growth allowance, or mask the fit surfaces.
- Under hard anodizing, masking is usually the more reliable choice for H7 bores and fine threads.

How much each anodizing type grows
Type II anodizing
Sulfuric acid anodizing, often called Type II under MIL-A-8625, converts the aluminum surface into a hard oxide layer. A typical coating is about 8 to 25 µm. Roughly half of that grows outward and half penetrates into the base metal, so a part with a 12 µm coating grows about 6 µm per surface. A bore with that coating shrinks in diameter by about 12 µm.
Type II anodizing can be dyed black, red, blue, gold and many other colors. Color consistency depends on the alloy: 6061 gives a clean, even result, 7075 tends to look slightly warmer, and high silicon cast alloys can look gray or blotchy. If several parts must match in color, ask for them to be anodized in the same batch, or agree on an approved color sample.
Type III hard anodizing
Hard anodizing produces a thicker, denser layer, commonly 25 to 60 µm, with much higher wear resistance. It suits sliding surfaces, pneumatic components, guide blocks and parts that see repeated handling. The trade-offs are size change, color and cost. With a 50 µm hard coat, each surface grows about 25 µm, which is enough to turn a slip fit into an interference fit. Natural hard anodize is gray to bronze in color, and dark colors are the most reliable choice when dyeing.
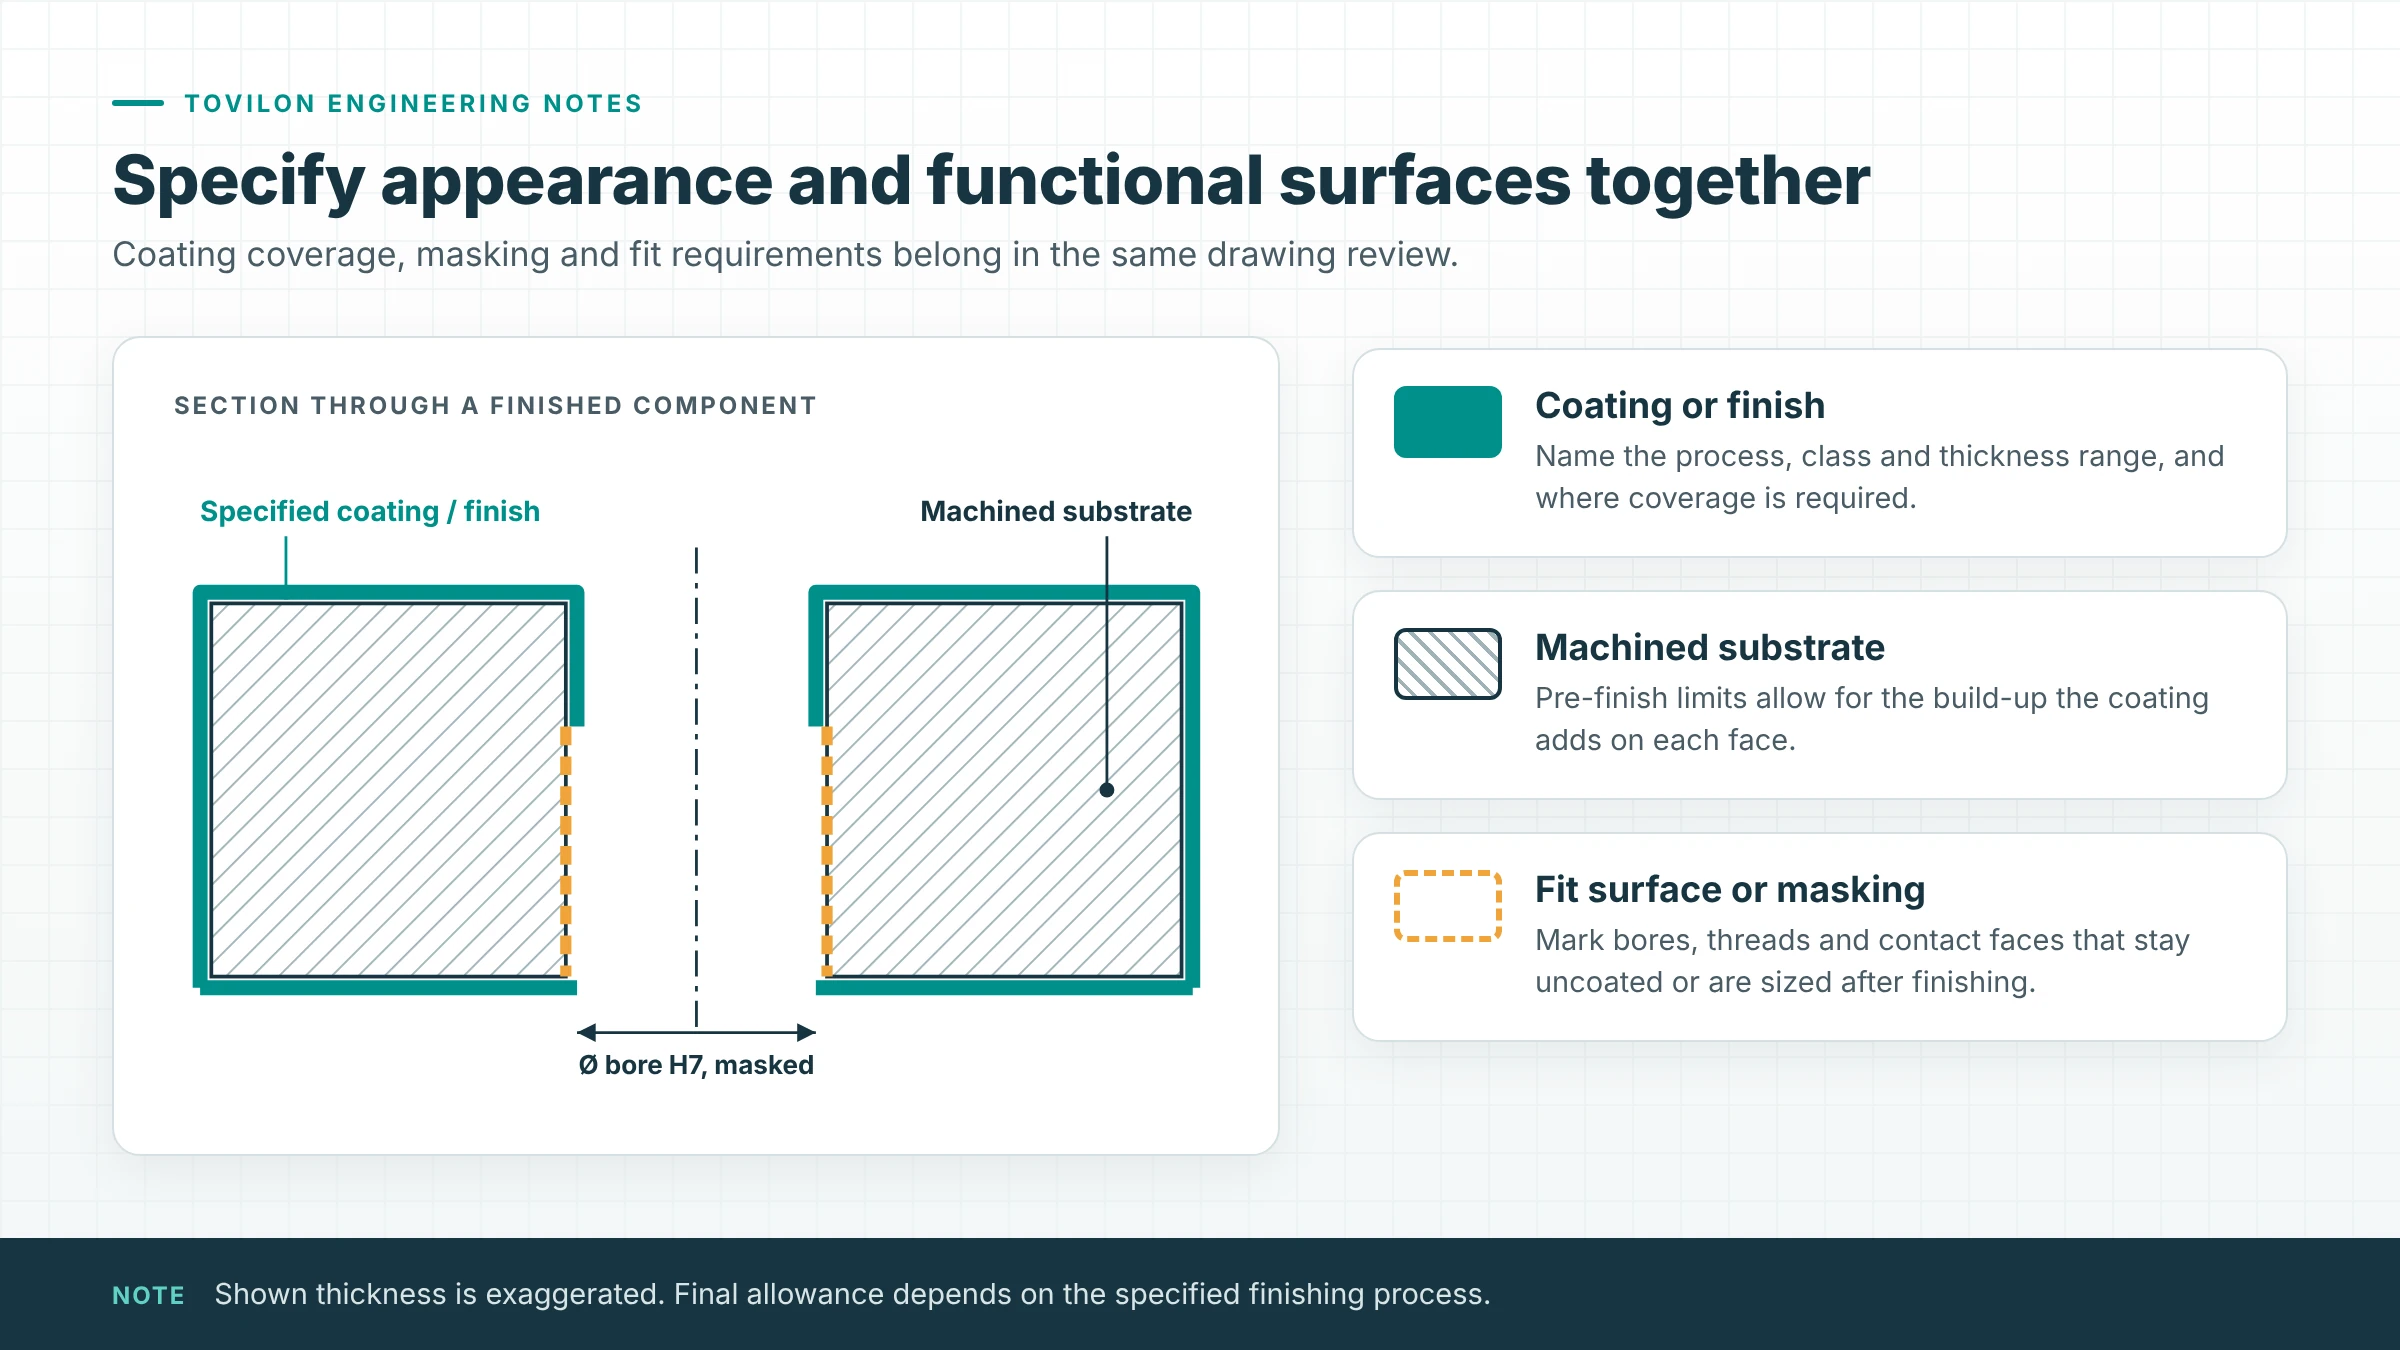
For close fits, there are two common approaches. Machine external diameters undersize and internal diameters oversize by the agreed coating growth allowance, so they reach final size after coating, or mask the fit surfaces and leave them bare. The drawing should state which dimensions apply after finishing.
Worked example: machining allowances for anodized fits
The examples below show what the coating does to a real fit and what size the feature has to be machined to before finishing. They assume the coating grows about half its thickness outward on each surface, a common rule of thumb; the anodizer can confirm the actual growth for your alloy and process.
| Feature, size after finishing | Coating thickness | Effect on the feature | Machine before finishing to | Tolerance left for machining |
|---|---|---|---|---|
| Bore Ø20 H7 (20.000 to 20.021 mm) | Type II, 10 to 15 µm | Diameter shrinks 10 to 15 µm | 20.015 to 20.031 mm | 16 µm of the original 21 µm |
| Bore Ø20 H7 (20.000 to 20.021 mm) | Hard anodize, 45 to 55 µm | Diameter shrinks 45 to 55 µm | 20.055 to 20.066 mm | 11 µm; masking is usually the better choice |
| Shaft Ø20 g6 (19.980 to 19.993 mm) | Type II, 10 to 15 µm | Diameter grows 10 to 15 µm | 19.970 to 19.978 mm | 8 µm of the original 13 µm |
| Internal thread M6 × 1, 6H (pitch diameter tolerance 150 µm) | Type II, 10 to 15 µm | Pitch diameter shrinks about 20 to 30 µm | Tap normally, or use an oversize tap for close fitting threads | About 120 µm; usually workable |
| Internal thread M6 × 1, 6H | Hard anodize, 45 to 55 µm | Pitch diameter shrinks about 90 to 110 µm | Not practical by sizing alone | Mask with plugs or fit inserts after finishing |
Two lessons follow. First, the variation in coating thickness consumes part of the fit tolerance, so the machining band before finishing is always tighter than the drawing band. Second, the thicker the coating, the more that variation dominates. For H7 bores and fine threads under hard anodizing, masking is usually cheaper and more reliable than pre-compensating the machined size. State the coating thickness range on the drawing, and whether each critical dimension applies before or after finishing.
Threads and anodizing
Threads are where coating thickness causes the most trouble. On a 60° thread form, the pitch diameter changes by about four times the coating build-up on each flank. A Type II coating that adds 6 µm per surface can therefore shift the pitch diameter by more than 20 µm, enough to make a fine thread bind. The practical options are to mask tapped holes with plugs, chase threads after anodizing, or specify threaded inserts installed after finishing. Mark masked threads clearly on the drawing rather than relying on a general note.
Masking or pre-compensation: how to choose
Pre-compensate the machined size when the coating is Type II, the thickness range is agreed with the anodizer, and the tolerance left after subtracting the coating variation is still practical to machine. It also suits fit surfaces that need the coating for corrosion protection.
Mask the surface when the coating is hard anodizing on an H7 bore or a fine thread, when the coating variation would consume most of the tolerance, or when the surface must stay bare: bearing seats, grounding points and some sealing faces.
For threads, the options are plug masking, chasing the thread after anodizing (which removes coating from the flanks), or fitting threaded inserts after finishing. Inserts are the most robust choice for fasteners that are often removed.
Whichever route is chosen, state on the drawing whether each critical dimension applies before or after finishing, and list the masked surfaces.
What to write on the drawing
A finish note that can be quoted and inspected usually includes the following:
- Finish type and specification, for example Type II anodize per MIL-A-8625, black
- Coating thickness range, where it matters
- Color or approved appearance sample, and whether batch matching is required
- Masked surfaces: tapped holes, bearing bores, grounding points, sealing faces
- Whether dimensions apply before or after finishing
- Roughness requirements on identified faces only
- Cosmetic zones and acceptable handling marks, especially on visible parts
Common mistakes we see on drawings
The most frequent issue is a tight H7 bore on a part marked “hard anodize” with no masking or post-finish note. The second is a general “anodize black” note on a part made from an alloy that will not anodize to a deep, even black. The third is a color requirement with no reference sample, which leaves appearance acceptance open to interpretation. Each of these is easy to resolve during drawing review, and much harder after parts are finished.
Other finishes for machined aluminum
Before choosing a finish name, decide what the surface needs: corrosion protection, wear resistance, electrical conductivity, a cosmetic color, or simply a clean, burr-free face. A robot arm cover, a sensor bracket inside a cabinet and a sliding guide block can all be 6061 aluminum, yet each needs a different treatment. When the function is stated, alternatives can be suggested. When only a finish name is given, it is quoted exactly as written, even if a cheaper or more suitable option exists.
As machined
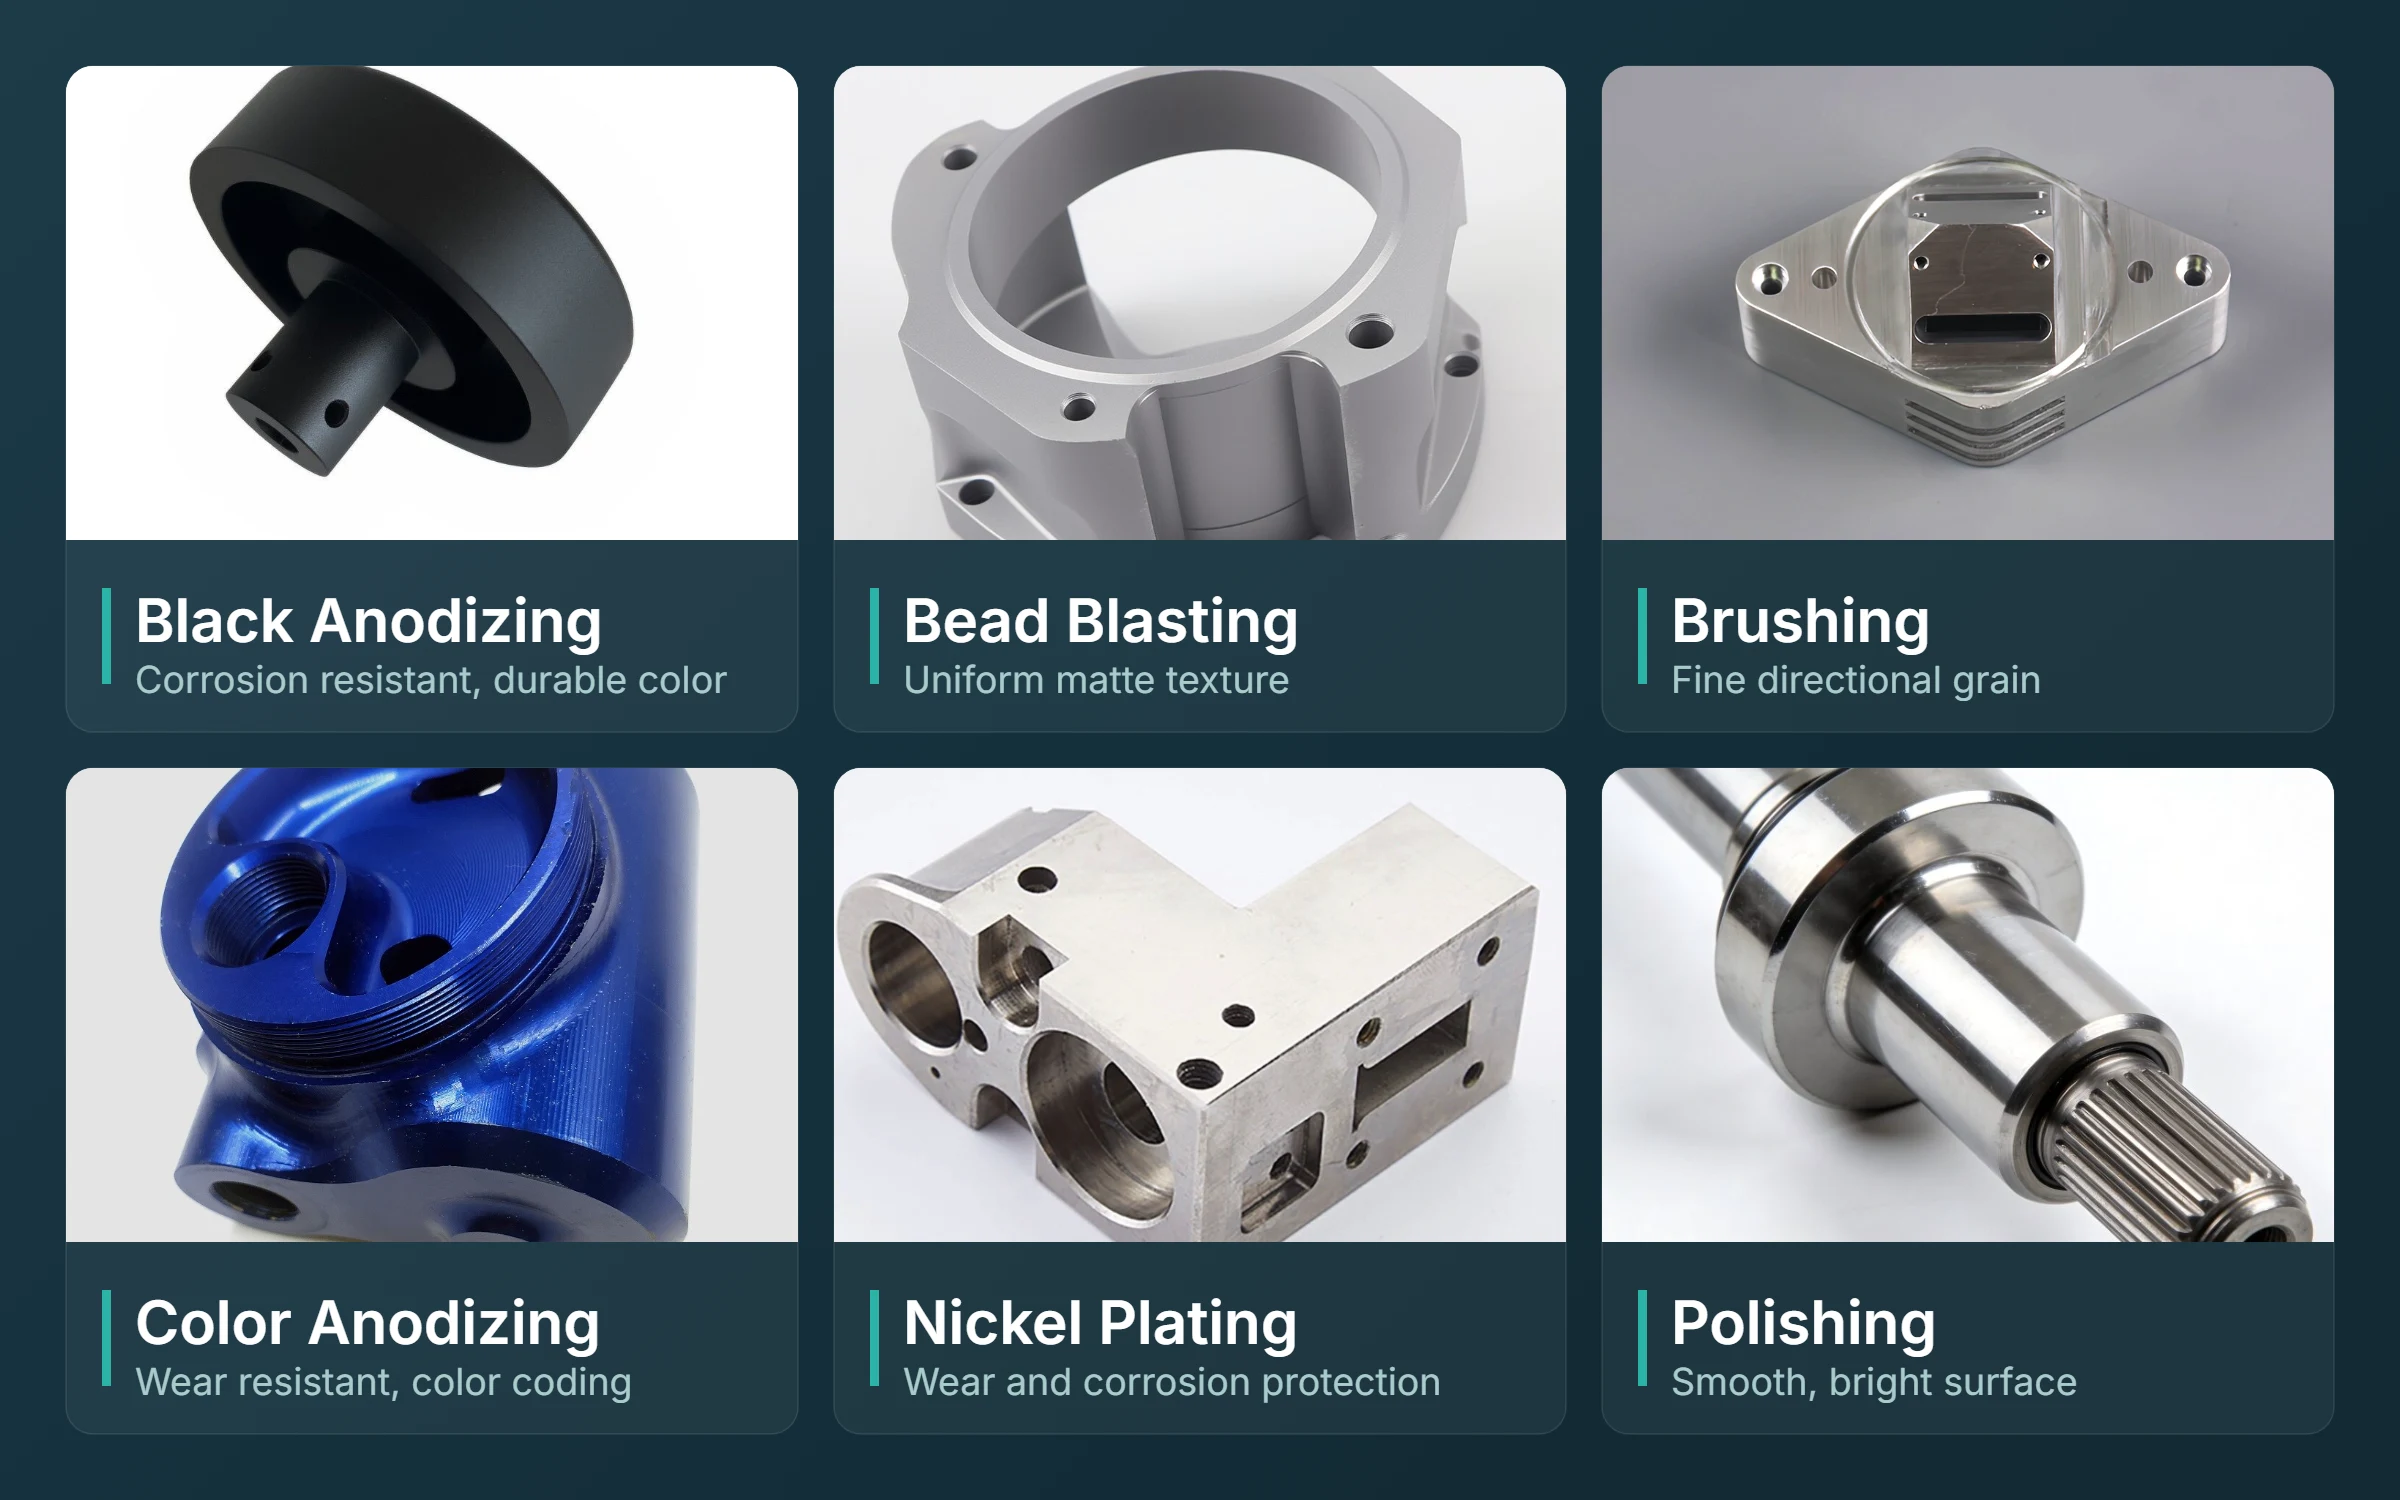
An as-machined surface keeps the tool marks from milling or turning. Typical values are around Ra 3.2 µm for general milled faces and Ra 1.6 µm or better where finishing passes are specified. It is the lowest cost choice and adds no thickness, which makes it a sensible default for internal brackets, fixture plates and prototypes. Aluminum does form a thin natural oxide, but it is not enough for humid, salty or outdoor environments.
Bead blasting
Bead blasting gives a uniform matte texture and hides light tool marks. It is purely cosmetic. It does not improve corrosion resistance on its own and it can slightly round sharp edges and soften fine features. Blasting is usually combined with anodizing for the even satin look seen on consumer and industrial products. If precision faces, sealing surfaces or threads must stay sharp, mark them as masked.
Chromate conversion coating
Chromate conversion coating, often referred to by the trade name Alodine or by MIL-DTL-5541, leaves a very thin film with almost no measurable dimensional change. It protects against corrosion, works well as a primer for paint and, in its Class 3 form, keeps the surface electrically conductive. That makes it a common choice for electronics housings, grounding points and EMI shielding faces. Appearance ranges from clear to light gold. Trivalent versions are now widely used where hexavalent chromium is restricted, and the drawing should state which type is acceptable.
Electroless nickel plating
Electroless nickel deposits an even coating, typically 5 to 25 µm, that follows the shape of the part, including inside bores and threads. It offers good wear and corrosion resistance and a bright or satin metallic look. Because the build-up is uniform, it is easier to predict than anodizing on complex geometry, but it still has to be accounted for on fits. Phosphorus content affects hardness and corrosion resistance, so state the class if your application depends on it.
Powder coating and painting
Powder coating gives a thick, durable colored finish, usually 50 to 120 µm. It is well suited to covers, frames and external panels, and poorly suited to precision features. Fits, threads, grounding points and mating faces are normally masked. Edges and inside corners can collect more coating, so cosmetic zones and functional zones should be identified separately.
Polishing
Polishing improves appearance and can lower roughness on visible faces. It also removes a small amount of material and can round edges. Specify which faces are to be polished and the target appearance, rather than writing “polish all over” on a part that also has precision bores.
Quick comparison
| Finish | Typical thickness | Main benefit | Watch out for |
|---|---|---|---|
| As machined | None | Lowest cost, no size change | Limited corrosion resistance |
| Bead blast | None (removes slightly) | Uniform matte look | Softens edges, cosmetic only |
| Type II anodize | 8 to 25 µm | Corrosion resistance, color | Bore and thread size change, alloy color variation |
| Type III hard anodize | 25 to 60 µm | Wear resistance | Large size change, limited colors |
| Chromate conversion | Negligible | Conductive corrosion protection, paint base | Lower wear resistance |
| Electroless nickel | 5 to 25 µm | Uniform coating, wear resistance | Fits must allow for build-up |
| Powder coat | 50 to 120 µm | Durable color on large surfaces | Masking required on precision features |
More on fit allowances and finishes
For choosing a finish by what the surface has to do, across aluminum, steel and plastics, see materials and surface finishes. For how bearing seat fits and hole position tolerances change the machining and inspection route, see the bearing seat and hole pattern tolerance guide.