Internal corner radii
Use radiused internal corners where an end mill must reach.
CNC MILLING
CNC milling services for aluminum housings, brackets, mounting plates and fixtures, from 1 piece to repeat batches. On multi-face and complex milled parts, the number of setups is often one of the main cost drivers, so it is one of the first things we look at on your drawing, together with tool access to angled and curved features.
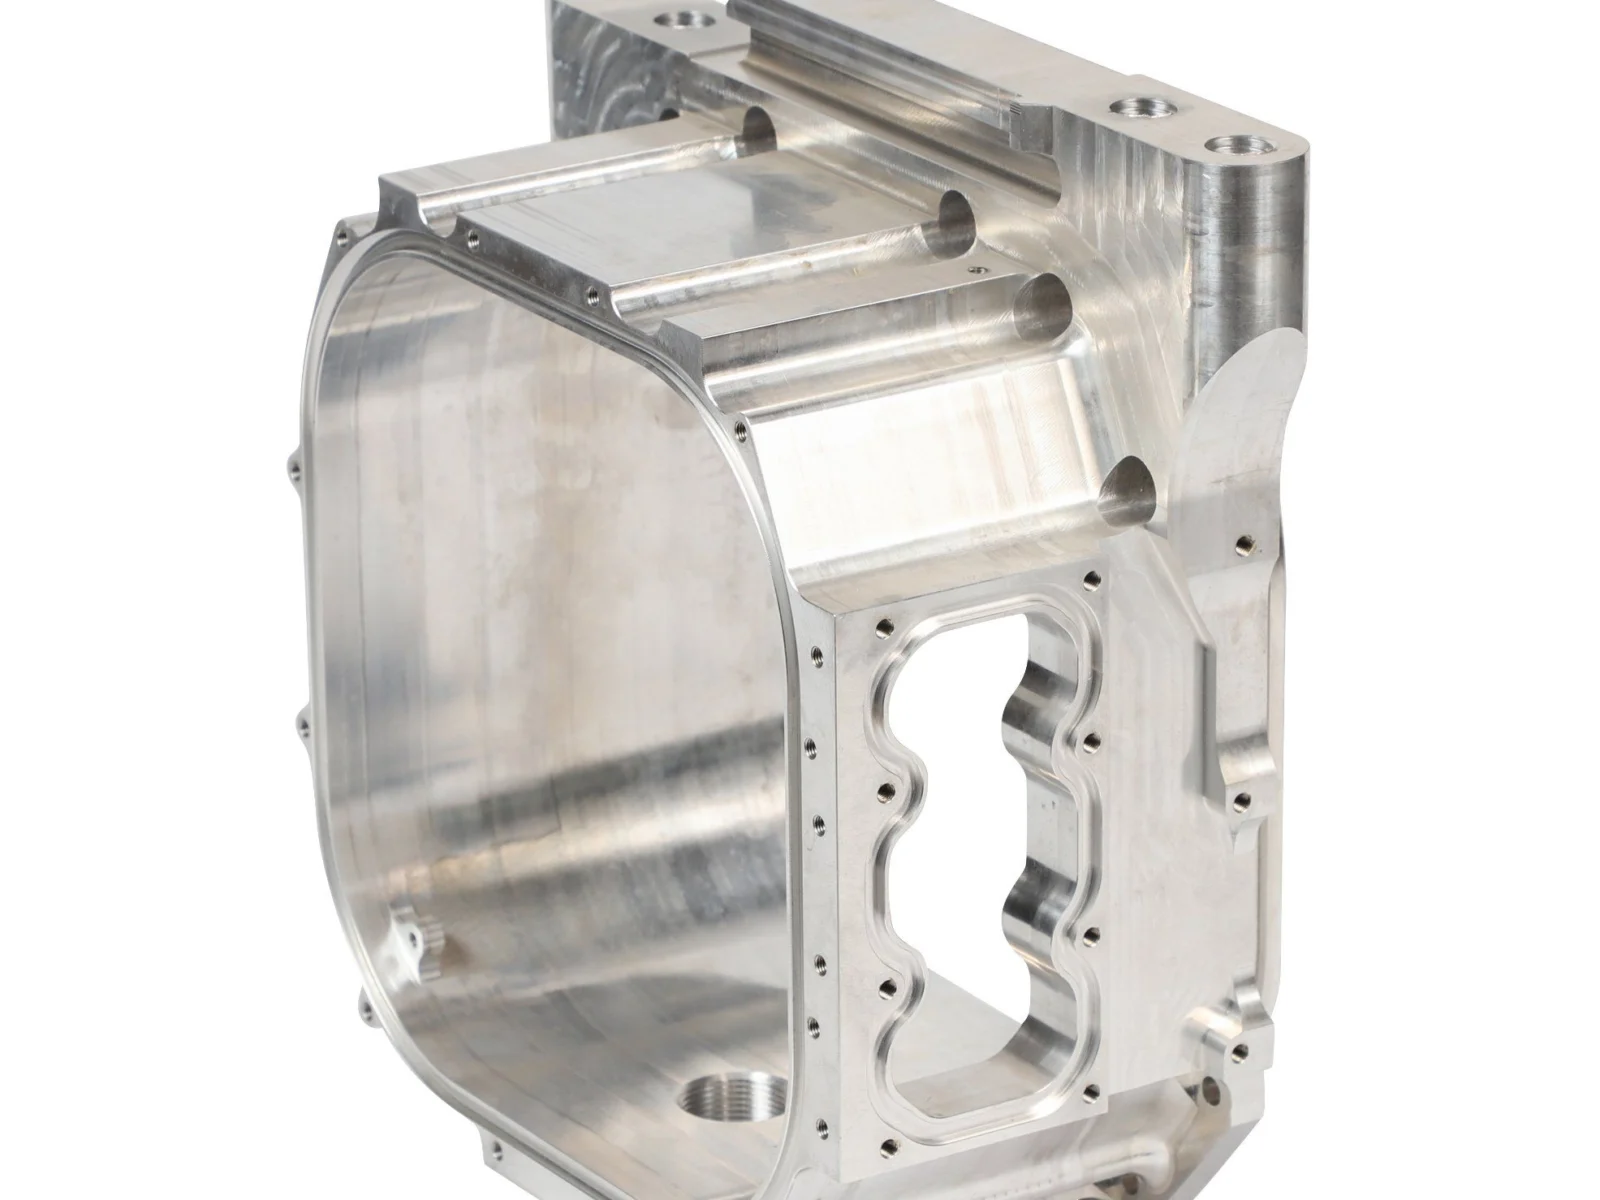
TYPICAL MILLED PARTS
Specify pockets, hole patterns and mounting faces for equipment housings, robot plates and assembly tooling.

Pockets, through-cuts and hole patterns machined from plate.

Machined interfaces aligned to your assembly.

Bosses, bores and hole patterns machined on angled faces.

Pockets, bores and mounting interfaces machined to the drawing.

Locating and workholding parts for manufacturing.

HOLES & THREADS
Drilling creates the holes required for mounting, locating and assembly. Hole sizes, depths, thread requirements and the relation to machined datums are reviewed against the drawing. Milling, drilling and tapping are coordinated within the part route.
DESIGN FOR MILLING
Use radiused internal corners where an end mill must reach.
Review deep pockets and thin walls for deflection and workholding.
Call out the datums that control assembly fit.


ALLOYS & FINISHES
Aluminum offers an effective balance of machinability and weight for many milled parts. Stainless steel, carbon steel, brass, and engineering plastics may be more suitable for wear, corrosion, conductivity, or insulation needs.
Milled parts are planned around the faces and bores that control assembly. We decide the number of setups, the fixture and the datum transfer before programming, so related features are cut from the same reference wherever the geometry allows. Typical values are listed below; the tolerance for each feature is confirmed during drawing review.
Part examples made to drawing: a robot joint housing in 7075, an automation fixture with locating pins and anodized aluminum pocket cases.
Parts up to 2500 × 2000 × 900 mm on gantry machining centers. Large frames and plates are reviewed for fixturing, stress relief and inspection access before quotation.
When bores, faces or bosses on several sides must stay aligned, or when the part has angled features and curved surfaces. Cutting them in one clamping avoids the position error that builds up across separate fixtures, although a 3-axis route with a dedicated fixture is sometimes cheaper, so both are compared when quoting.
Aluminum 6061, 6082 and 7075, stainless steel 304 and 316, carbon and alloy steels, brass, and engineering plastics such as POM and PEEK. Hardened inserts are finished by wire EDM or grinding after heat treatment.
We rough the part, release it from the fixture so internal stress can relax, then finish critical faces. Wall thickness, cutter reach and internal corner radii are reviewed with you during the quotation.
A STEP model and a PDF drawing with the revision, material, quantity, finish and the datums that control assembly. An engineer replies with questions or a quotation within one business day.
LET’S TALK ABOUT YOUR PART
Mark the faces and bores that locate in the assembly. We will come back with the likely number of setups and the tolerances that affect the price most. Or email the drawing to info@tovilon.com.